WhatsApp: +8615665767071 Email: info@eworldmachine.com
 English

Views: 0 Author: Site Editor Publish Time: 2026-10-14 Origin: Site
Edge quality dictates the success of premium glass fabrication. Achieving a flawless, optically clear edge consistently requires precise capital equipment tailored to your specific production demands. Mismatching a glass polishing machine to your shop's actual operational needs introduces severe financial and operational risks. Incorrect spindle configurations or selecting the wrong machine architecture directly causes production bottlenecks, excessive polishing wheel wear, and sub-standard edge finishes characterized by micro-chipping, delamination, or dull surfaces.
This technical evaluation framework helps fabricators and plant managers align specific edge profile requirements, daily throughput demands, and facility constraints with the correct machinery. By systematically analyzing material types, volume expectations, and mechanical features, operators can eliminate guesswork and implement a highly efficient edge processing line that meets strict quality standards without unnecessary overhead.
Spindle Count Dictates Polish Quality: The number of spindles directly correlates with the ability to achieve a flawless, optically clear finish in a single pass; complex edges require higher spindle counts.
Machine Architecture Must Match Output: Straight-line edgers maximize throughput for standard flat glass, while CNC centers or shape edgers are mandatory for custom, curved, or multi-profile architectural glass.
Consumables Drive Long-Term Costs: The initial capital expenditure is only part of the investment; evaluating the machine's compatibility with standard diamond, resin, and felt wheels is critical for controlling operational costs.
Slurry Management is Non-Negotiable: Effective water filtration and cerium oxide recovery systems are required to protect machine components and maintain consistent polishing friction.
Software Integration is the New Standard: Modern glass polishing machines must integrate with shop floor ERP/MES systems to track linear meter output, wheel wear, and overall equipment effectiveness (OEE).
Table of Contents
Glass edging machines must support the required edge profile, including flat, pencil, beveled, and bullnose edges. Flat edging focuses on safe handling and smooth finishing, while pencil edges require rounded polishing wheels. Beveled and bullnose profiles demand precise angle control and stable grinding pressure. Selecting suitable equipment ensures consistent edge quality and finishing accuracy.
Glass edging machine selection depends on the material being processed. Laminated glass requires controlled grinding pressure and cooling to protect interlayers, while glass intended for tempering needs smooth, defect-free edges. Low-E glass requires scratch-resistant handling, and thick architectural glass demands heavy-duty transport systems.
Glass Type | Main Processing Challenge | Recommended Machine Feature |
|---|---|---|
Laminated Glass | Heat buildup and interlayer damage | Adjustable speed and effective cooling |
Glass for Tempering | Edge micro-cracks | Progressive grinding and fine polishing |
Low-E Coated Glass | Coating scratches | Non-marking conveyors and clean coolant |
Thick Architectural Glass | Heavy loads and vibration | Reinforced transport and stable machine frame |
Explore Eworld's glass edging and polishing machines for different glass processing requirements.
Glass edging machine production capacity should be evaluated by processing speed, linear meters per hour, and changeover efficiency. High-volume factories benefit from continuous operation and automated controls, while smaller workshops require flexible adjustments for different glass sizes and edge profiles. Matching equipment capacity to actual production demand helps improve efficiency and control operating costs.
Glass thickness and weight capacity directly affect edging machine stability and processing accuracy. Thick architectural glass requires reinforced conveyors, durable bearings, and rigid machine structures to prevent vibration and misalignment. Thin glass needs precise pressure control, fine grinding wheels, and stable transportation to minimize cracking and edge chipping.
Straight-line edgers represent the workhorse of the flat glass industry. Their primary application is high-speed, high-volume flat edging and arrissing. Glass panels are loaded vertically onto an in-feed conveyor and pass through a series of stationary grinding and polishing spindles. When evaluating this category, operators must scrutinize track durability and conveyor speed variability. The transport pads must grip the glass securely without causing surface damage. Modern units utilize motorized thickness adjustments controlled via PLC, eliminating the tedious manual cranking required on older mechanical models.
Double-edging machines process two parallel edges simultaneously, making them the optimal solution for maximum throughput applications like shower doors, commercial partitions, and appliance glass. Because the glass moves horizontally through two opposing banks of spindles, the synchronization accuracy between the two sides is paramount. If the tracks run at slightly different speeds, the glass will skew, resulting in out-of-square panels. Buyers must evaluate the footprint requirements, as these machines demand significant floor space, and assess their capability to integrate seamlessly into fully automated production lines with robotic loading and unloading systems.
Custom fabrication, curved glass, and intricate beveling require shape edging machines. These units utilize a rotating vacuum table or a multi-axis arm to maneuver the glass against the grinding head. The evaluation focuses on the articulation of the grinding head and template tracking accuracy. Semi-automatic models rely on physical templates to guide the grinding path, while advanced versions utilize digital tracking. Fabricators must weigh the trade-offs between manual control, which offers tactile feedback for delicate custom pieces, and semi-automatic control, which provides better consistency for small production runs.
CNC glass processing centers handle complex, multi-step fabrication requiring routing, drilling, milling, and edging on a single horizontal bed. These machines eliminate the need to move glass between different workstations, drastically reducing handling damage and labor costs. When evaluating a CNC center, software compatibility is the primary concern. The machine must integrate smoothly with standard CAD/CAM software to translate architectural drawings into machine code quickly. Buyers must assess tool-change speed and the reliability of the vacuum pod system, which must hold the glass absolutely rigid against the aggressive torque of routing tools.
Selecting a reliable glass edging machine requires evaluating spindle configuration, polishing systems, automation, and safety features. These factors directly influence glass edge quality, production efficiency, and long-term operating costs. Explore Eworld's glass edging and polishing machines for different processing requirements.
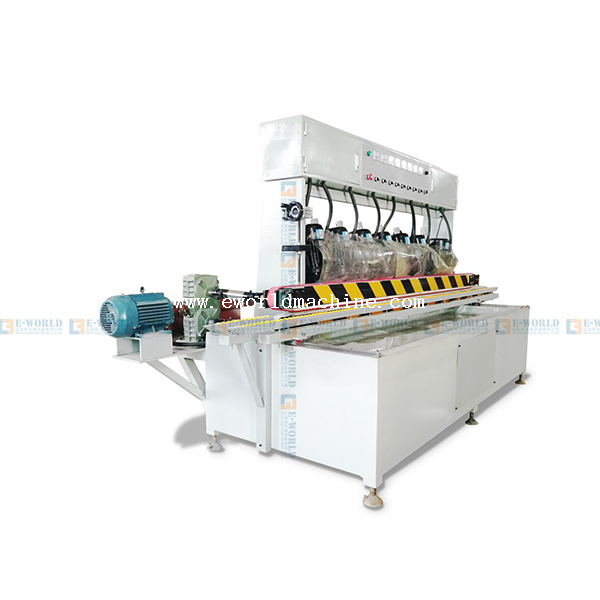
Glass edging machine spindle count determines grinding and polishing capabilities. Basic 4-spindle machines suit simple edge processing, while 8–11 spindle configurations support progressive grinding, chamfering, and high-gloss polishing. More spindles allow different grinding wheels to share the workload, improving edge consistency and production efficiency.
Glass polishing wheel compatibility affects edge quality and consumable costs. Pneumatic pressure systems provide adjustable polishing force, while mechanical systems may require more frequent adjustment. Machines supporting widely available diamond, resin, and polishing wheels offer greater flexibility and can simplify replacement and maintenance.
Automated glass edging machines use PLC controls, touchscreen interfaces, and adjustable processing parameters to improve consistency. Depending on the model, advanced features may include wheel wear compensation, production monitoring, and factory system integration. These capabilities help reduce manual adjustments, improve productivity, and support preventive maintenance.
Glass edging machine safety features should include emergency stops, protective enclosures, suitable electrical protection, and interlocked access doors where applicable. Effective coolant management and safe glass handling also reduce workplace hazards. Buyers should verify relevant safety certifications and compliance requirements for their target market.
Installing a glass edging and polishing machine requires planning for production space, water management, electricity, and operator training. Proper facility preparation supports safe material handling, stable machine performance, and efficient workflow integration.
Glass edging machine installation requires adequate space for equipment, glass loading, unloading, and maintenance. Factories should consider maximum glass dimensions, conveyor length, and material handling equipment when planning the layout. Sufficient clearance improves workflow efficiency and reduces handling risks.
Glass edging water filtration systems remove abrasive glass particles and polishing residues from circulating coolant. Effective filtration helps prevent clogged water lines, premature component wear, and poor edge finishes. Closed-loop water treatment can also reduce water consumption and support responsible slurry disposal.
Glass edging machine energy consumption depends on spindle quantity, motor power, and operating conditions. Energy-efficient motors and variable frequency drives (VFDs), where available, can help optimize electricity usage. Buyers should verify power requirements and evaluate water recycling systems to reduce operating costs.
Glass edging machine operator training should cover equipment settings, polishing wheel adjustments, safety procedures, and routine maintenance. CNC equipment may also require programming knowledge. Clear operating instructions and manufacturer-supported training help reduce errors, improve productivity, and maintain consistent glass edge quality.
Purchasing a glass edging machine requires balancing equipment capabilities, production demand, consumable costs, and technical support. Buyers should evaluate long-term operating expenses rather than focusing only on the initial machine price.
Glass edging consumables, including diamond grinding wheels, resin wheels, and polishing materials, contribute to ongoing operating expenses. Their replacement frequency depends on glass thickness, processing volume, and machine settings. Estimating consumable costs helps manufacturers calculate realistic production expenses.
CNC glass edging machines offer advanced processing flexibility but may not be necessary for every factory. Smaller workshops handling mainly straight-edge glass can often benefit from simpler multi-spindle edging equipment. Choosing machinery based on actual production needs helps avoid unnecessary investment.
Glass edging machine after-sales support is essential for minimizing downtime. Buyers should confirm spare parts availability, maintenance documentation, remote assistance, and technician support before purchasing. Reliable service access helps reduce repair delays and maintain production continuity.
Preventive maintenance for glass edging machines includes daily cleaning of conveyors and water nozzles, weekly inspection of grinding wheels and lubrication systems, and periodic checks of spindle alignment, bearings, and filtration components. Following manufacturer-recommended maintenance schedules helps prevent unexpected breakdowns and maintain consistent edge quality.
Map your daily linear meter output and most frequent edge profiles to determine the exact spindle count and machine architecture required.
Request a live demonstration or send sample glass to the manufacturer to verify edge quality and machine stability under real-world conditions.
Audit the manufacturer's warranty, local spare parts inventory, and field technician availability before issuing a purchase order.
Design your facility floor plan to accommodate the full in-feed and out-feed footprint, including space for closed-loop water filtration systems.
A: Achieving a premium, high-gloss flat edge typically requires an 8 to 11 spindle configuration. This allows for a proper progression from coarse diamond roughing to fine resin grinding, finishing with felt wheels and cerium oxide for maximum optical clarity.
A: Standard straight-line edgers are designed specifically for flat edges and arrissing. Producing pencil or bullnose profiles requires specialized peripheral wheels and a machine architecture designed to accommodate the specific wrap-around grinding action, such as a dedicated shape edger or a CNC center.
A: Diamond wheels handle aggressive stock removal and rough shaping. Resin wheels utilize finer abrasives to remove diamond scratches and smooth the edge. Felt wheels, used in conjunction with cerium oxide slurry, provide the final chemical-mechanical polish to achieve a transparent, glossy finish.
A: While the machine itself may be 6 meters long, you must account for the in-feed and out-feed zones. Processing 3-meter glass panels requires at least 3 meters of clearance on both ends, resulting in a minimum total linear footprint of 12 meters.
A: Wheel lifespan varies heavily based on glass thickness and wheel quality. Segmented diamond wheels process tens of thousands of linear meters, while softer polishing resins require replacement every 2,000 to 5,000 linear meters. Tracking wear rates is essential for budget planning.
A: Yes, for high-volume operations. A closed-loop system with a centrifuge removes abrasive glass dust from the coolant. Without it, recirculated glass particulate destroys spindle bearings, clogs water lines, and severely degrades the quality of the final edge polish.
 简体中文